Shearing Machine Company Tips for Maintaining Consistent Cut Quality in Sheet Metal
2026-10-23
Maintaining consistent cut quality in sheet metal isn’t just about having a good shearing machine—it’s about knowing what to check before every run. From blade clearance and rake angle to material clamping and backgauge repeatability, small oversights can quickly turn into burred edges or out-of-tolerance parts. At HUNSONE, we’ve spent years helping shops troubleshoot these exact issues, and we’ve distilled that experience into a practical set of tips. Whether you’re chasing a cleaner edge on stainless steel or trying to reduce scrap on aluminum, the following guide will walk you through the adjustments and habits that make the biggest difference. No fluff—just the details that keep your cuts crisp, square, and consistent from the first sheet to the last.
Why Blade Clearance Drifts and How to Correct It
Blade clearance rarely stays put for long in high-speed rotating equipment. Thermal growth is the usual first culprit—casings and rotors expand at different rates during startup, so a gap that measures fine at ambient temperature can tighten or open up once things get hot. Add in centrifugal force stretching the rotor, and you’ve got a clearance that shifts by a few thousandths of an inch before anyone notices.
Another overlooked cause is uneven casing distortion. If the machine sits on an uneven foundation, or if piping loads pull on the flanges, the casing can go slightly oval. That means the blade tips see a variable gap around the circumference—acceptable at one position, dangerously tight at another. Vibration from imbalance or misalignment makes it worse, wearing down the tips and gradually increasing the running clearance, which then bleeds efficiency.
Correcting drift starts with measuring what’s actually happening during operation. Proximity probes or laser-based tip timing give a real-time picture of the gap under load, not just during a cold shutdown. From there, you can adjust the cold clearance setpoint to account for known thermal growth, or switch to a more stable casing design with better ribbing. For the foundation or piping issue, a proper soft-foot check and alignment correction often brings the clearance back into a consistent band without touching the blades themselves.
The Dull Blade Problem That Ruins Cut Tolerance
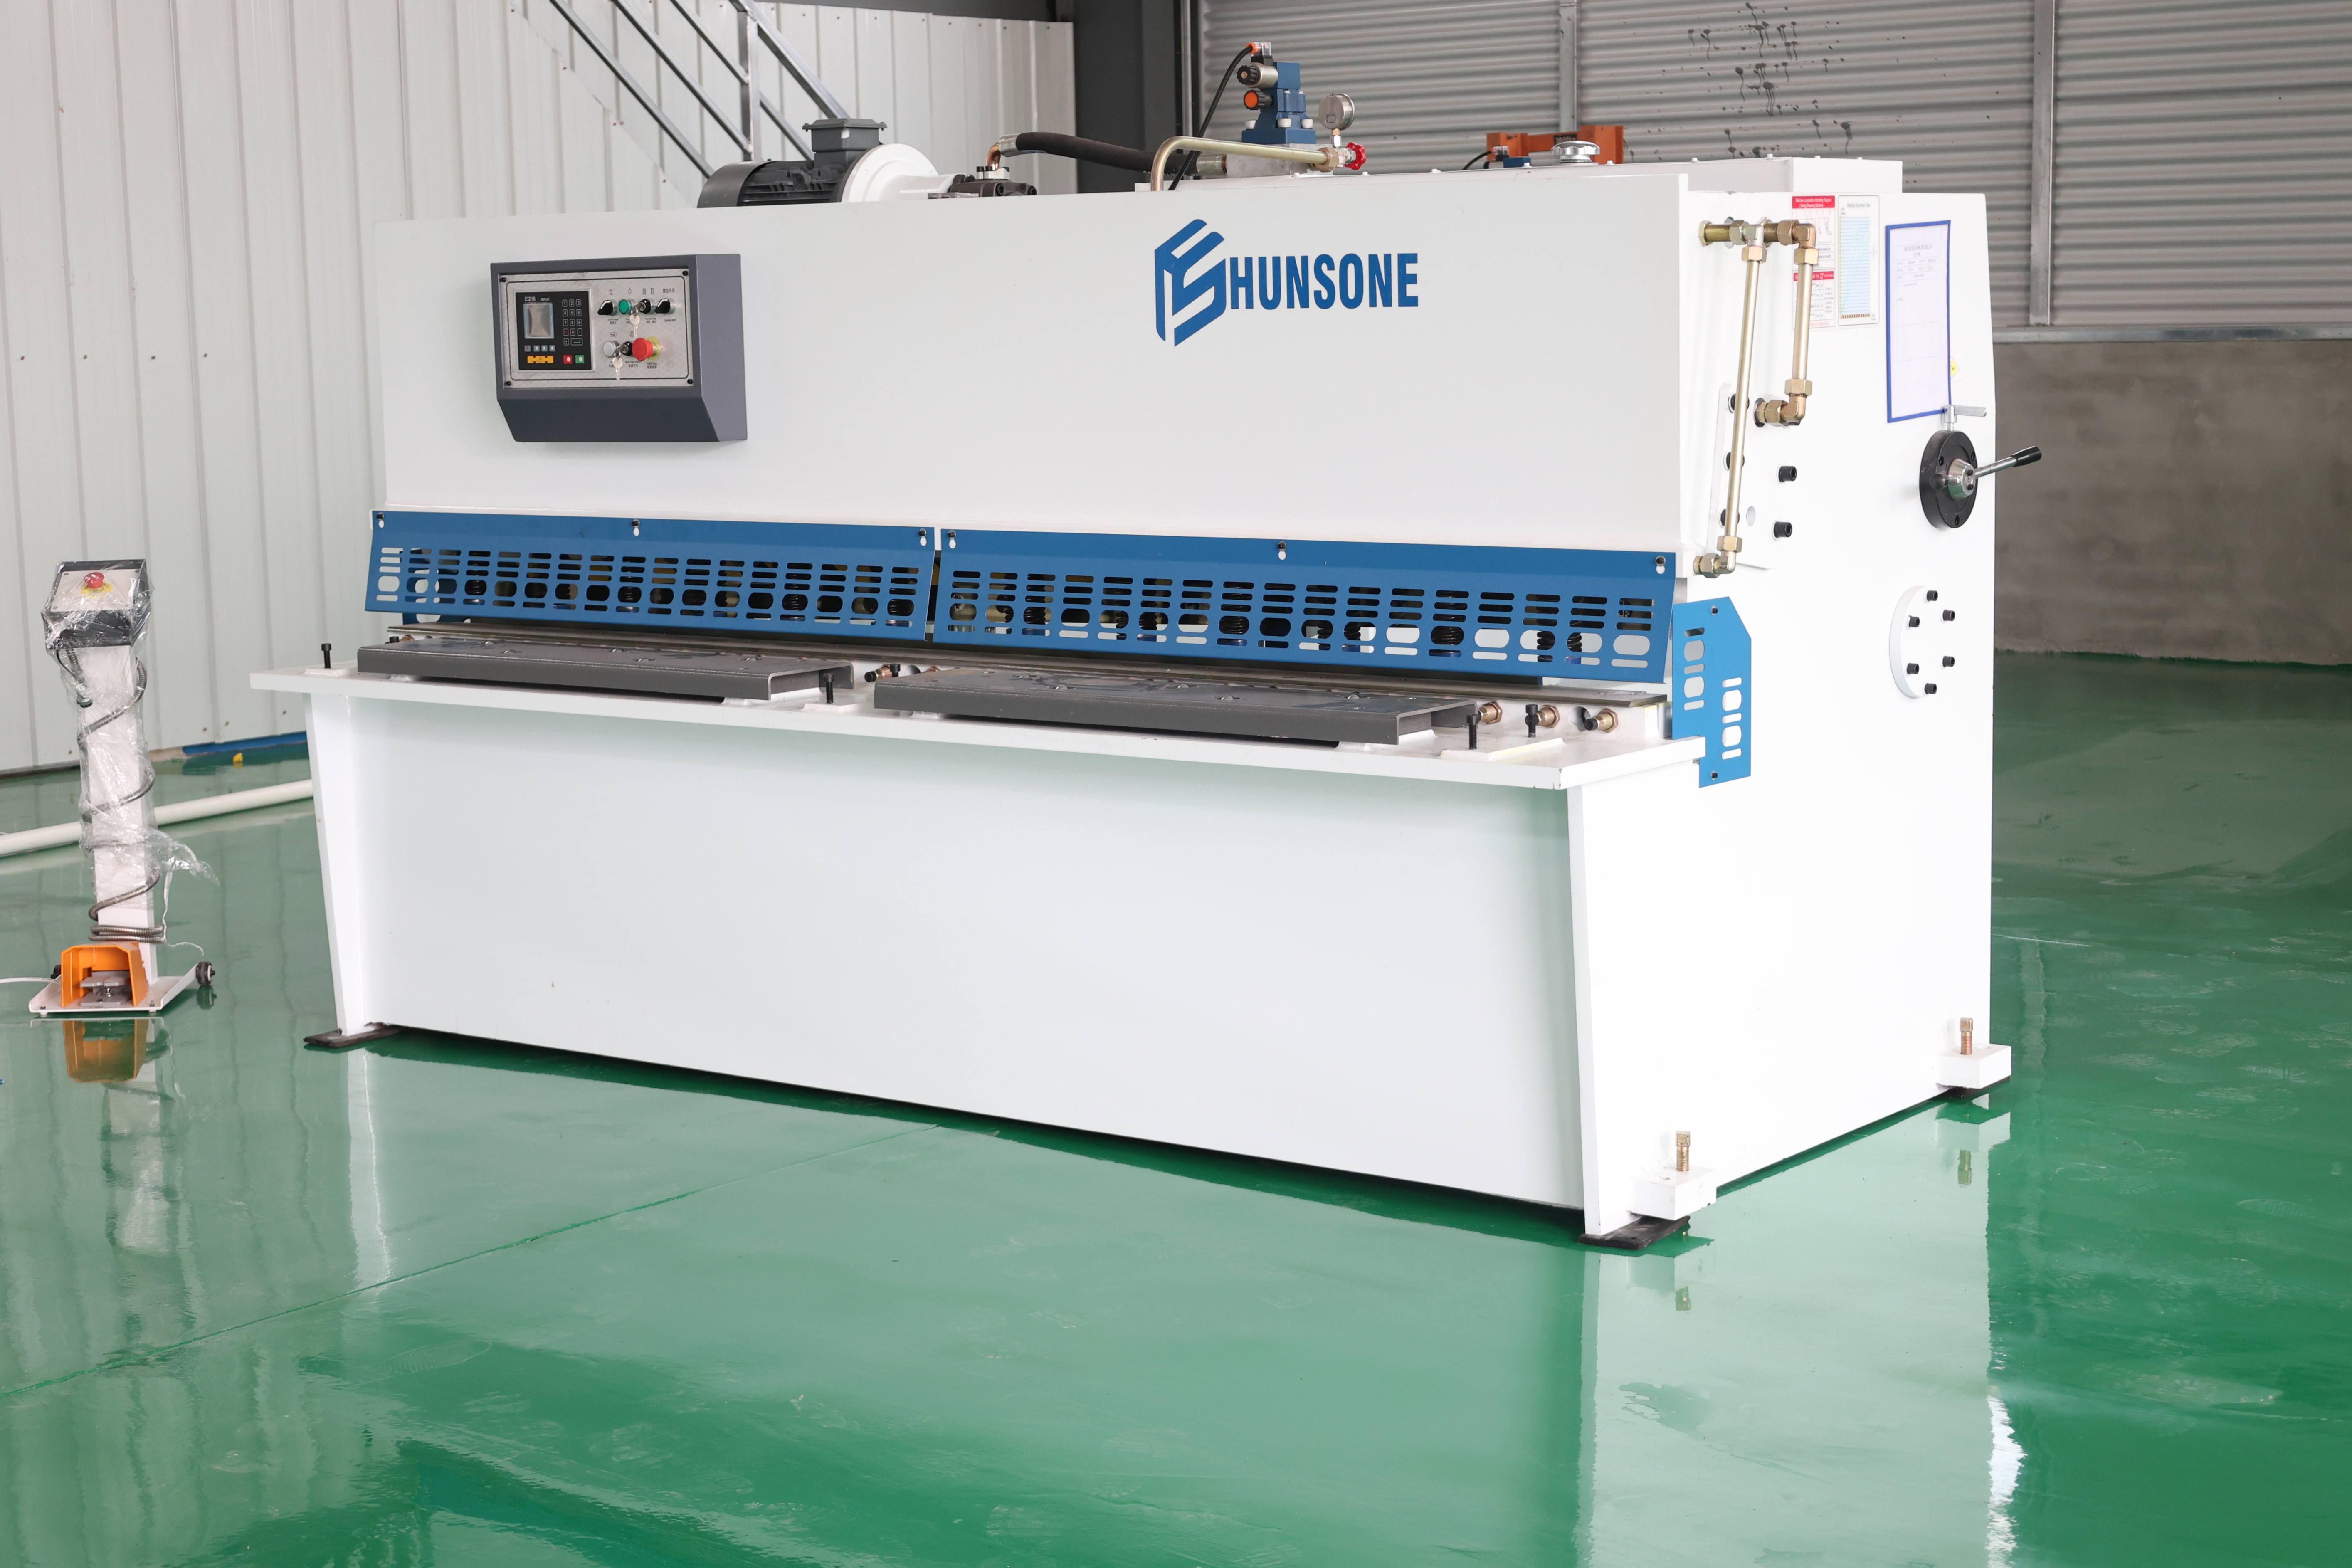
A blade that has lost its edge does more than slow the cut. It starts to push material instead of slicing through it, which shifts the kerf and leaves edges that wander off the intended line. Over a long run, this drift shows up as parts that measure consistently out of spec, even when the machine settings haven't changed.
The real trouble is that dullness rarely announces itself. Operators may notice a slight increase in feed pressure or a rougher finish, but those signs are easy to dismiss until tolerance failures appear. By then, the tool has already been forcing the material to deflect, creating tapered cuts or burnished sidewalls that no amount of post-processing can fully correct.
Keeping cut tolerance tight means treating blade condition as a variable, not an afterthought. Regular inspection, scheduled sharpening, and tracking cut counts per edge are far cheaper than scrapping a batch or reworking parts that a dull blade quietly pushed out of range.
Clamping Force Errors That Warp Thin Sheet Metal
Thin sheet metal rarely forgives a careless clamp. A fraction too much pressure on one corner, a clamp jaw that bites harder on the leading edge than the trailing one, or a fixture that holds the sheet rigidly while the cutting tool pulls across it—any of these can leave behind a visible warp or a subtle bow that only shows up during assembly. The problem is that sheet metal, especially aluminum alloys and high-strength steels under about 3 mm thick, has very little stiffness in the flat direction. Once you exceed the local yield point, the metal doesn't spring back; it takes a new shape.
The most common clamping errors start with over-tightening. Operators often assume that a tighter clamp means a more secure part, but on thin stock, that extra torque simply bends the unsupported span between clamp points. Uneven clamp spacing creates its own distortion pattern: areas with close-spaced clamps stay flat while the wider gaps bow upward, especially during milling or routing. Another frequent mistake is placing a clamp directly over a hollow or unsupported region—like a pocket or a rib—where the metal can flex under the pad instead of being backed by a solid surface. Even the clamp type matters; a steel C-clamp with a small flat pad concentrates force in a small area, whereas a broad, soft-faced toggle clamp spreads the load. All of these errors introduce internal stresses that release immediately as warpage or later as delayed distortion after the part is removed from the fixture.
Preventing clamp-induced warpage is less about acquiring exotic equipment and more about rethinking the workholding sequence. Start by supporting the sheet metal on machined flat parallels or a vacuum table whenever possible, so the clamping force has something solid to press against. Use torque-limiting wrenches or preset pneumatic clamps to keep force consistent across multiple points, and space clamps symmetrically around the part rather than clustering them on one side. For very thin or large sheets, consider adhesive workholding, low-melt alloys, or magnetic chucks that distribute holding force evenly without point loading. The key is to test a first article carefully: measure flatness after unclamping, not while the part is still constrained. If a fixture routinely warps thin sheet metal, the fix is usually not more clamping force—it's smarter distribution of the force you already have.
Lubrication Shortcuts That Leave Marks on Sheet Metal
Using a penetrating oil or general-purpose spray lubricant instead of a dedicated forming fluid is a common shortcut that quickly backfires. The light solvents in these products flash off under pressure, leaving bare metal sliding against the die. The result is a series of fine score lines or a bright, polished streak right where the punch first contacts the sheet.
Another tempting move is to over-lubricate or to randomly coat only the die surface. Excess lubricant gets pushed ahead of the forming area and trapped in small cavities, creating localized hydraulic pressure that distorts the panel. This shows up as orange-peel texture, dull patches, or even small dents near bends and draw beads.
Even the application method matters more than most realize. Wiping oil on with a shop rag deposits lint and airborne grit that get pressed into the metal, leaving pinpoint pits or embedded specks. Dirty, recycled oil is worse because it carries metal fines from previous jobs, turning the lubrication step into a source of scratches rather than a safeguard.
Backgauge Drift as a Hidden Cause of Off-Size Cuts
A backgauge that gradually loses its reference position can turn a perfectly calibrated cutter into a source of scrap. Operators often notice the problem only after measuring finished parts and finding them a millimeter or two short, with no obvious change in setup. Because drift tends to accumulate over dozens or hundreds of cycles, early batches may pass inspection while later ones fall outside tolerance, making the root cause frustratingly easy to miss.
Common contributors include worn lead screws, loose encoder couplings, insufficient brake torque on the positioning motor, or thermal expansion during sustained runs. Even a few thousandths of an inch of movement per stroke compounds into visible size variation by the end of a shift. Diagnosing the issue requires logging actual backgauge position during cycling rather than relying only on commanded values, since many controllers display the intended target instead of the measured location.
The fix often involves tightening mechanical components, re-homing the axis more frequently, or adding a closed-loop scale that verifies position after every move. Replacing a tired brake or upgrading to a servo with active holding torque can also eliminate movement after the backgauge reaches its set point. Once drift is controlled, off-size cuts that seemed random usually disappear, confirming that the hidden drift was the real source of variation.
A 15-Minute Morning Routine for Repeatable Shearing
Stretch your hands and shoulders before touching a blade. A few slow wrist circles and finger flexes wake up the small muscles that guide the comb. Then run through the first three positions on a fence rail or a dummy—no sheep, just the motion. The point isn't speed; it's making the first real pull feel like the fiftieth.
Gear comes next, but not the way most people do it. Instead of just grabbing the handpiece, check comb tension by feel and give the crank one drop of oil. Lay out the blades in the order you'll use them. These little checks take ninety seconds, but they remove the variables that make one shearing day sharp and the next one sloppy.
Finish with a slow mental rehearsal. Close your eyes and picture the sheep's shoulder against your knee, the way the fleece opens under the comb, the exact line of the first blow. Breathe out once, and don't open your eyes until the whole sequence runs through. That quiet minute does more for repeatability than any amount of coffee.
FAQ
Check blades at least once per shift or every 8 hours of continuous use. Run a fingernail lightly along the cutting edge—if it catches or feels rounded rather than crisp, it’s time for sharpening or replacement.
A general starting point is 5% to 10% of material thickness, with thinner gauges leaning tighter and thicker plates needing slightly more gap. Always verify with a test cut and adjust in small increments until the edge shows a clean shear line without excessive burr.
Twisting usually comes from uneven blade clearance, dull spots on the blade, or feeding the sheet at a slight angle. Make sure the backgauge is square, the hold-downs apply even pressure, and the material rests flat against the table before each cut.
Keep blade clearance matched to material thickness, use sharp blades, and don’t force the machine beyond its rated capacity. Lightly deburring with a file or deburring tool after the cut is also normal for many shops, but heavy burrs signal a setup or wear issue.
Proper lubrication reduces friction and heat at the blade contact points, which helps maintain a stable cutting gap. Follow the manufacturer’s schedule for oiling or greasing, but avoid over-lubricating, as excess oil can attract metal fines and affect hold-down grip.
Calibrate the backgauge at least once a month, or whenever you notice length inconsistencies greater than your acceptable tolerance. Use a precision square or calibrated test strip to verify that the gauge returns to the same position after repeated cycles.
Store sheets flat or on proper racks to avoid warping, and handle them with clean gloves or lifting tools to prevent surface contamination. Before shearing, wipe the material free of debris, oil, or mill scale that could interfere with blade contact.
Yes. Feed the sheet smoothly without jerking, keep your hands clear of the cutting zone, and avoid stacking multiple sheets unless the machine is rated for it. Consistent foot pedal or CNC trigger operation prevents partial strokes that can leave uneven edges.
Conclusion
Maintaining consistent cut quality on a shearing machine rarely comes down to a single dramatic fix—it is the accumulation of small, often invisible adjustments. Blade clearance drifts from repeated impacts and thermal cycling, so checking and resetting it against the material thickness chart before each shift prevents burrs and edge rollover. A dull blade is just as damaging; it forces the machine to work harder and widens the tolerance band, so touch-up honing or timely replacement should be part of the weekly schedule. Clamping force also deserves attention, especially on thin sheet metal, where excessive pressure can bow or warp the workpiece and produce cuts that look straight but measure out of square.
Lubrication shortcuts leave residue and drag marks on the sheet surface, so use only the manufacturer-recommended lubricant and wipe the bed and hold-downs clean between batches. Backgauge drift, often caused by loose fasteners or worn bearings, quietly shifts dimensions, so verifying the backgauge against a calibrated scale every morning catches this before it becomes an off-spec order. A fifteen-minute routine that combines blade clearance checks, backgauge verification, clamping pressure review, and quick lubrication inspection gives operators a repeatable baseline. These habits, applied together, keep cut edges clean, tolerances tight, and thin material flat—without relying on luck or last-minute corrections.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/