Video Measuring Machine: How to Choose the Right One for Your Needs
2026-10-02
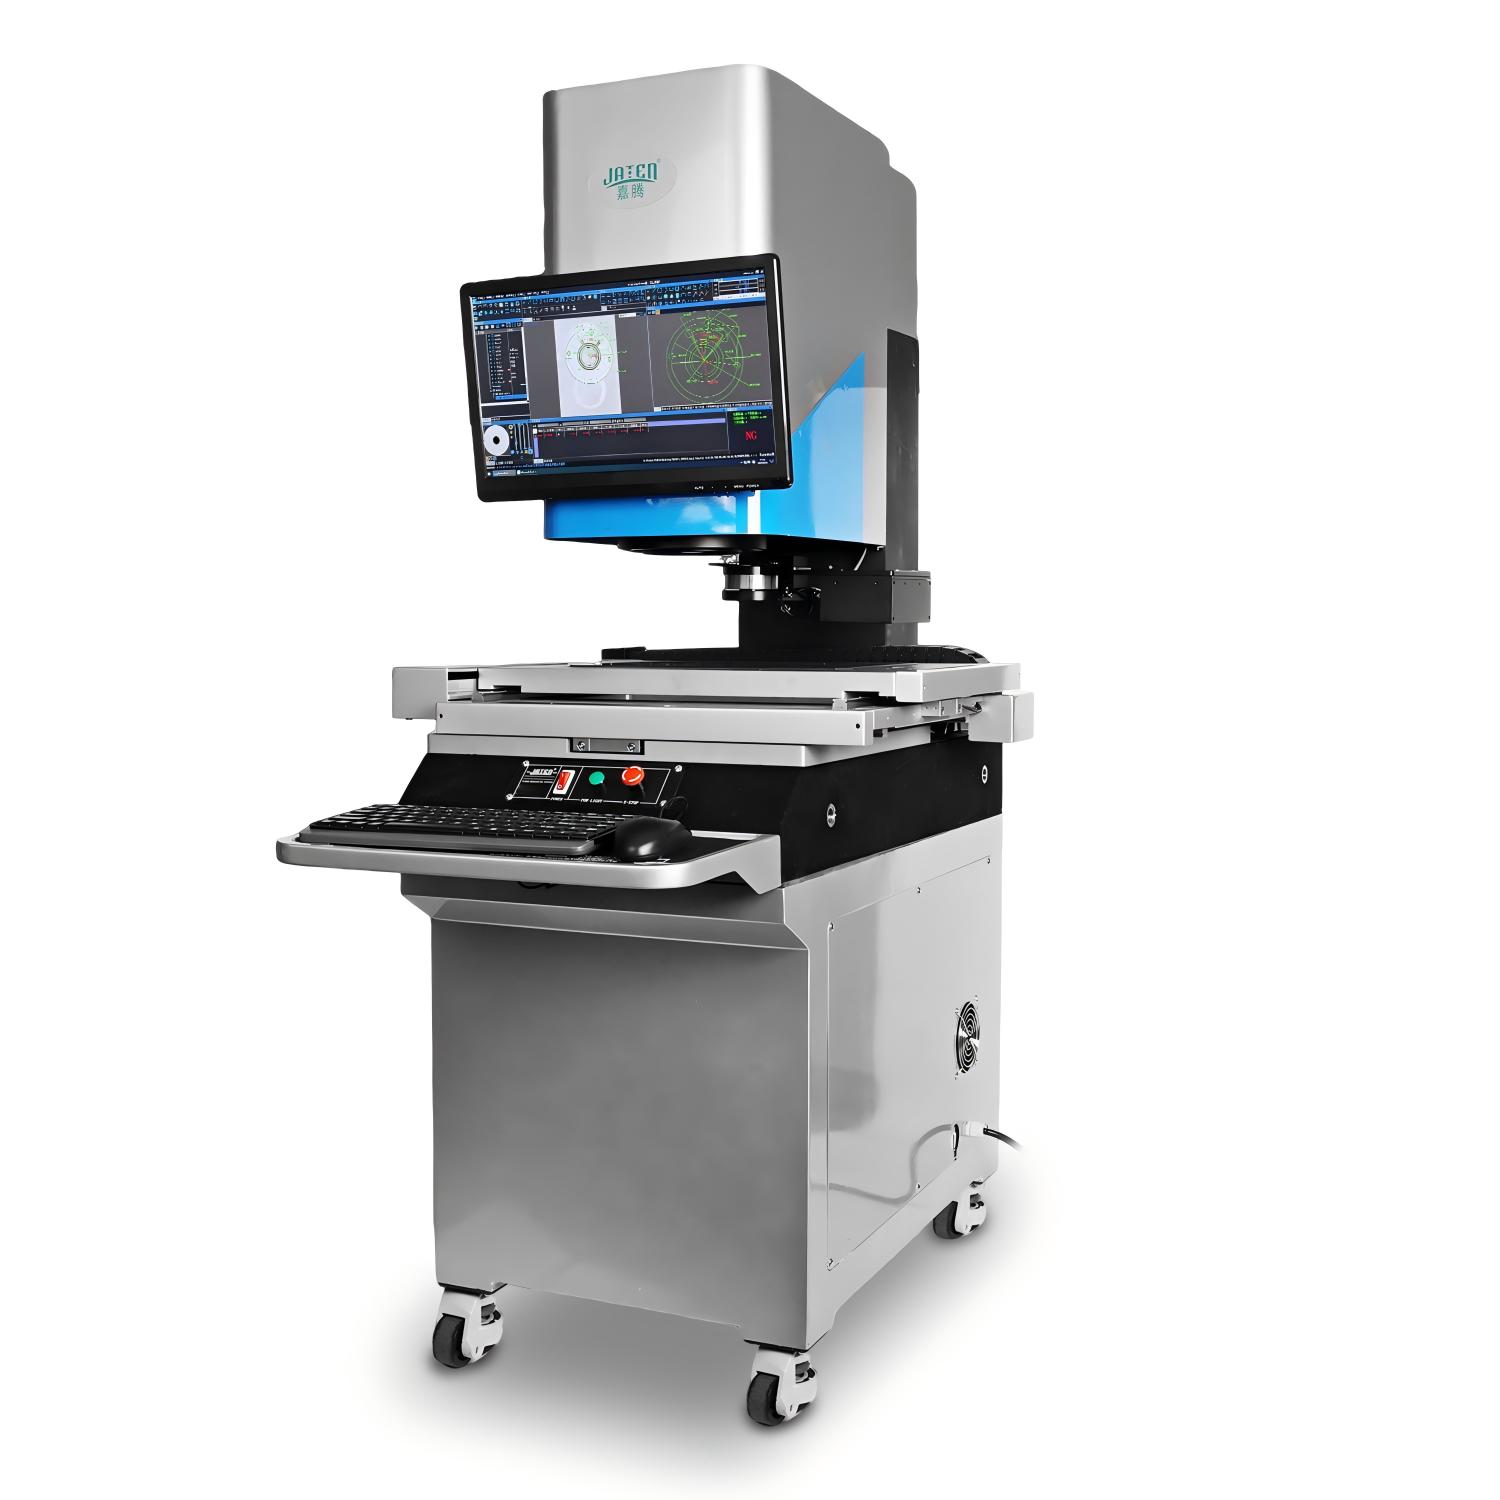
Selecting a video measuring machine can feel like navigating a maze of pixel counts, stage sizes, and software add-ons. The right choice isn’t just about the highest resolution—it hinges on your part geometry, tolerance requirements, and throughput expectations. In this guide, we’ll break down the factors that actually matter, from optical zoom range to illumination control, so you can avoid costly over-specification or underperformance. And if you’re looking for proven, application-focused systems, JATEN offers a range of VMM solutions designed to meet real-world inspection demands. Let’s get you from spec sheet confusion to confident measurement.
Define Your Accuracy Needs in Real Numbers
Vague promises like "highly accurate" fall apart the moment you need to act on a prediction. Instead, attach a tolerance to every performance claim—say, weekly demand forecasts must land within ±6% of actuals, or a fraud model should keep false positives under 2 per 1,000 transactions. These numbers force conversations about what you can tolerate operationally and financially.
A practical way to set the target is to trace the cost of any unit of error. If each 1% gap in pricing accuracy shaves $8,000 off quarterly margin, then an acceptable error band becomes obvious: you might allow 1.5% if the cost of further tuning exceeds the saving. Historical variability helps too—look at past model errors and choose a threshold that beats the best manual process by a clear margin, such as cutting median absolute error from 12% to 9%.
Once set, treat the metric as a living number. Review it quarterly against changing data drift, customer tolerance, and operating conditions. If a model consistently delivers 4% error when the requirement is 5%, consider tightening the target; if it wobbles above 5% in certain regions, split the metric by segment rather than accepting a misleading average.
Choose a Stage Size That Leaves Room to Grow
A stage that fits today’s needs perfectly often becomes tomorrow’s constraint. Instead of measuring only for current gear and headcount, think about how your events evolve. Leave at least a few feet of unclaimed depth and wing space, and avoid pinning risers or cable runs to the very edges. That extra buffer keeps load-ins smoother when a last-minute speaker, live band, or larger screen gets added.
Modular staging and adjustable deck heights offer a practical way to keep flexibility without renting more space than you currently use. Look for layouts that can expand sideways or accommodate a thrust extension rather than committing to a fixed rectangle. This approach lets you test smaller setups now while preserving a clean upgrade path for higher attendance or more elaborate productions.
Also consider ceiling height, offstage storage, and access paths when sizing the stage. A platform that leaves room to grow isn’t just about square footage—it’s about how easily you can reposition monitors, add a backdrop, or route power without reworking the whole floor plan.
Compare Lighting Options Under Your Actual Part Conditions
When you evaluate lighting solutions on a spec sheet, the numbers often come from a clean, flat test target. Your production environment rarely works that way. A stamped metal bracket with oil residue, a dark plastic housing with subtle texture, or a highly reflective machined surface will each interact with light differently. What looks like a strong contrast in the lab can wash out or create glare when the part actually passes through your inspection station. That is why you need to compare options while the parts are moving at your line speed, mounted in the same orientation they will see in production.
Start by setting up a small test rig on your actual conveyor or fixture. Place two or three candidate lights—different geometries, wavelengths, or diffusion levels—at the same working distance. Run a batch of real parts, including the worst-case variations you know show up: parts with slight color shifts, oily fingerprints, or edge burrs. Capture images with your existing camera and lens, then look at the histogram and edge sharpness. A light that creates a nice even gray background on a clean sample might produce hot spots on a scratched surface. The only way to know is to watch the same flawed part travel under each light.
Don't rush this step. Many teams pick a light based on vendor demos with perfect parts, then spend weeks tuning the algorithm to compensate. Comparing under your actual conditions—with your part, your fixturing, your ambient light leaks—saves that rework. It also gives your integrator a clear record of what worked and what did not, so the final installation matches reality instead of a brochure photo.
Evaluate Software by Watching Someone Use It
Watching someone fumble through a new interface tells you more in five minutes than a stack of feature specs ever will. Instead of asking users what they think, sit beside them while they try to complete a real task. Watch where the mouse hesitates, which buttons get clicked by accident, and where their eyes drift when they're lost. These small, unguarded moments reveal the difference between software that feels obvious and software that just looks good in a demo.
The trick is to stay quiet and resist the urge to explain. If a tester asks, "What happens if I press this?" the honest answer is often another question: "What do you expect to happen?" Their guess, right or wrong, is a direct line into their mental model. Jot down every detour, every backtrack, and every sigh of frustration. Those are not failures of the user; they're pressure points in the design that no amount of polished onboarding will fix.
After a few sessions, patterns emerge that no survey would ever capture. Maybe everyone tries to drag a file into a window that doesn't accept drops, or they all miss the small settings icon tucked in the corner. That's when you stop polishing the surface and start fixing the underlying flow. Watching real people struggle is uncomfortable, but it's the fastest way to turn a clever piece of software into one that actually works.
Separate Must-Have Automation from Nice-to-Have
When deciding what to automate, many teams fall into the trap of treating every repetitive task as equally urgent. The result is a bloated automation roadmap that burns through developer hours without delivering meaningful relief. A more useful approach is to ask a blunt question: if this process never gets automated, will the business actually stop working? If the answer is yes, it belongs in the must-have bucket. If the answer is no, it might still be worth doing eventually, but it should not compete for the same resources.
Must-have automation usually protects revenue, keeps data consistent, or prevents a compliance failure. Think of invoice ingestion that feeds your accounting system without manual rekeying, or order synchronization between your storefront and warehouse. These are not glamorous, but they remove friction from core operations. Nice-to-have automation, on the other hand, often looks attractive in a demo but has a lower daily impact, like automatically generating a weekly report that nobody reads or sending welcome emails that could easily wait a day.
The practical way to split the two lists is to map each candidate process against the cost of failure and the frequency of use. A high-frequency task with a high error cost is a clear must-have. A low-frequency task with a soft failure mode can stay on the nice-to-have list for later. Revisit that list every quarter, because a task that was merely convenient last year can become essential as the business scales.
Look Past the Quote to Calibration and Support Costs
When comparing laboratory instruments, the initial purchase price rarely tells the whole story. Calibration expenses can quietly accumulate over time, especially for equipment that drifts or requires frequent adjustments to maintain accuracy. A unit with a lower upfront cost might need recalibration every few months, while a slightly pricier alternative holds its settings longer, reducing both downtime and recurring fees.
Support costs are another layer that often goes unnoticed until something breaks. Ask about response times, spare part availability, and whether technical assistance is included or billed per incident. Some manufacturers bundle years of proactive maintenance into the deal, while others charge extra for even basic troubleshooting. These ongoing obligations can dwarf the original quote within a couple of operational cycles.
To make a sound decision, request a detailed breakdown of calibration intervals and support tiers before signing anything. Factor in the cost of consumables, software updates, and any mandatory training. A transparent vendor will readily provide these figures, helping you see beyond the sticker price and understand what the instrument truly demands over its working life.
FAQ
It uses a camera and optical system to capture images of a part, then software measures dimensions, angles, and geometric tolerances without physical contact.
Look at the largest part you routinely inspect and add some margin. The stage travel and working distance need to cover that part without forcing you to reposition it too often.
Not necessarily. Match the machine's stated accuracy to your tightest tolerance. Paying for sub-micron capability you never use just inflates cost and can make the machine more sensitive to environment.
It's often the difference between a reliable edge and a blurry guess. Adjustable LED ring lights, coaxial light, and backlighting help handle different surface finishes and part geometries.
If you measure repetitive batches or need consistency across operators, yes. Features like CNC stage movement, auto-focus, and pattern recognition reduce human error and speed up inspection.
Software determines how quickly you can create measurement routines and export reports. Ask for a trial with your own parts to see if the interface feels natural and does not require constant workarounds.
Manual machines work for low volume and simple parts. CNC becomes worth it when you measure many identical parts or need programmed routines that run without an operator standing by.
A clean, temperature-stable area with minimal vibration gives you the most repeatable results. Even a good machine will drift if it sits next to a loading dock or under an air vent.
Conclusion
Choosing a video measuring machine starts with quantifying your accuracy requirements in real numbers—don't settle for vague terms like 'high precision.' Write down the tolerances your parts must meet, then look for a system that can measure at least one order of magnitude finer. At the same time, think about stage size not just for today's largest part, but for what you might measure in two years; a slightly larger granite base and travel range often costs less than upgrading later. Lighting is where many buyers go wrong, so bring a few of your most challenging parts—shiny, textured, or translucent—and test different illumination combinations under the same conditions you'd use on the shop floor.
Software evaluation should involve watching someone actually drive the interface for a real measurement routine, not just a canned demo. Ask yourself: can your team learn this in a week? Separate true automation needs—like CNC staging or pattern recognition for repetitive inspection—from features that sound impressive but won't get used. Finally, look past the initial quote and compare calibration intervals, service response times, and long-term support costs. A cheap machine that drifts out of spec or sits idle because calibration is expensive will cost far more over five years than a mid-range system with a solid support plan.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/